PLC and SCADA
PLC programming and SCADA development
We take on PLC programming for mechanical engineering and production, including with Beckhoff TwinCAT and Siemens TIA Portal, network machines and develop SCADA systems. The machine data comes together in a shared dashboard where your team reads the values directly.
PLC programming: programming controllers and networking machines
We program a single machine, connect several installations or evaluate your entire machine fleet together. We integrate new and existing machines as soon as their controller has a suitable interface. We check this on the installation beforehand.
Programming machine sequences
We develop and extend PLC programs for operating modes, step sequences, interlocks and peripherals. We program Beckhoff controllers with TwinCAT 3 and Siemens controllers in TIA Portal.
Connecting machines and acquiring data
We connect common controllers and bring together the available machine states, process values and production data. All data is then in one place.
A central overview of production
We develop SCADA systems for plant visualisation, central operation and production monitoring. Dashboards show states, faults and key figures across several machines.
Selected customers


Programming and extending PLCs
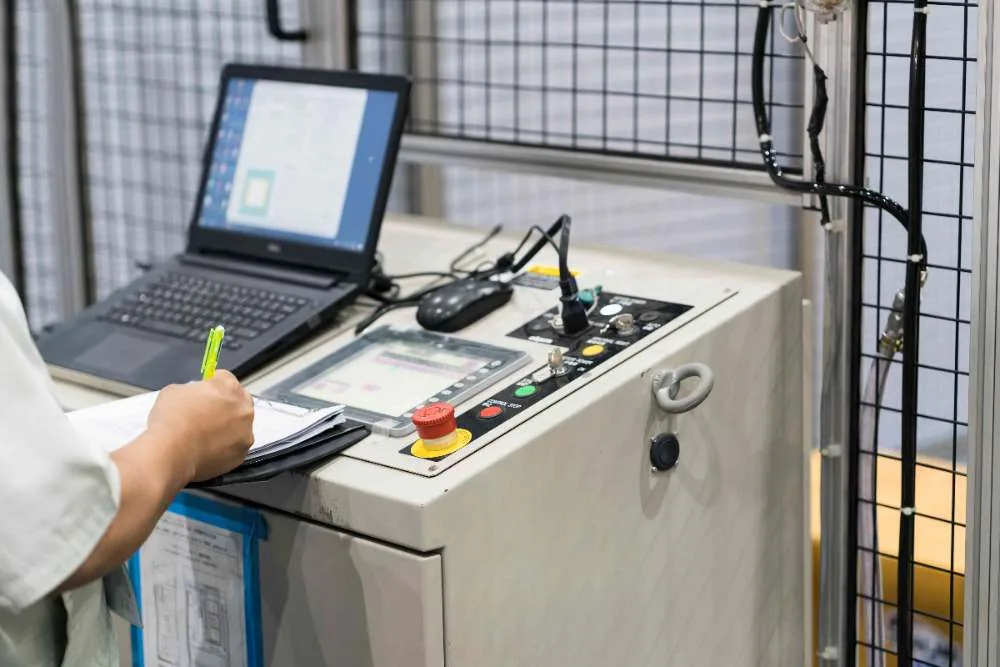
We write new PLC programs and extend existing controllers. Before programming, we define the scope of functions, interfaces and test cases together with you. At handover, you learn what was changed and why.
Sequence control
Developing operating modes, step chains, enables and interlocks to suit the machine and process.
Peripherals and stations
Integrating sensors, actuators and drives and coordinating handshakes and data transfers between controllers.
Operation and diagnostics
Programming recipes, messages, status displays and defined restart sequences for your team.
Commissioning and extension
Testing functions and fault scenarios on the installation, backing up program versions and documenting changes.
Beckhoff PLC programming with TwinCAT 3
We program Beckhoff controllers for machines and installations, either new or as an extension of an existing TwinCAT program. We clarify which controller and which TwinCAT version you use before we send you a quotation.
Beckhoff and TwinCAT are trademarks of Beckhoff Automation GmbH & Co. KG.
We program operating modes, step chains, interlocks and error handling in TwinCAT 3. We base the structure and designations on your program version.
We integrate EtherCAT terminals, sensors, actuators and drives into the controller and check every signal on the installation.
Siemens PLC programming in TIA Portal
We program Siemens controllers in TIA Portal for machines and installations, either new or as an extension of an existing program. We clarify which controller and which version you use before we send you a quotation.
Siemens and TIA Portal are trademarks of Siemens AG.
We program operating modes, step chains, interlocks and error handling in TIA Portal, and complex blocks in SCL. We base the structure and designations on your program version.
We back up the old version and implement the functions you need. We show how we upgrade older controllers such as S5 or S7-300 on our machine retrofit page.
Reprogramming or extending a controller?
Tell us the controller, installation and task. We will tell you how we would implement your project.
What we program controllers for
We program individual machines, robot cells and linked installations, both new and existing ones. The examples come from completed projects. Does your installation belong to a different group? Feel free to ask us.
Manufacturing and machining installations
Machines for producing, forming, machining and processing components. For a pipe manufacturer, we programmed safety and functional adjustments in the existing installation software.
Assembly and robotics installations
Assembly stations, robot cells and systems for feeding, joining and positioning. For a robotics application, we developed the software and commissioned the installation on site at the end customer.
Conveying, handling and packaging installations
Material transport, sorting, palletising and packaging. We program sequences, format changes and the transfers to adjacent stations.
Test benches and special-purpose installations
We build and program test benches for motors, pumps and gearboxes as well as visual inspection systems ourselves. For modular dosing stations and complete systems, we developed the PLC software.
Industries we program for
Automotive and suppliers, aviation, armaments and defence, mechanical and plant engineering, logistics and intralogistics, food and beverages, packaging, plastics, metalworking and metal processing, electronics and electrical engineering, medical technology and pharmaceuticals, chemicals, energy, and water and wastewater.
You will find further projects under References.
SCADA programming and plant visualisation
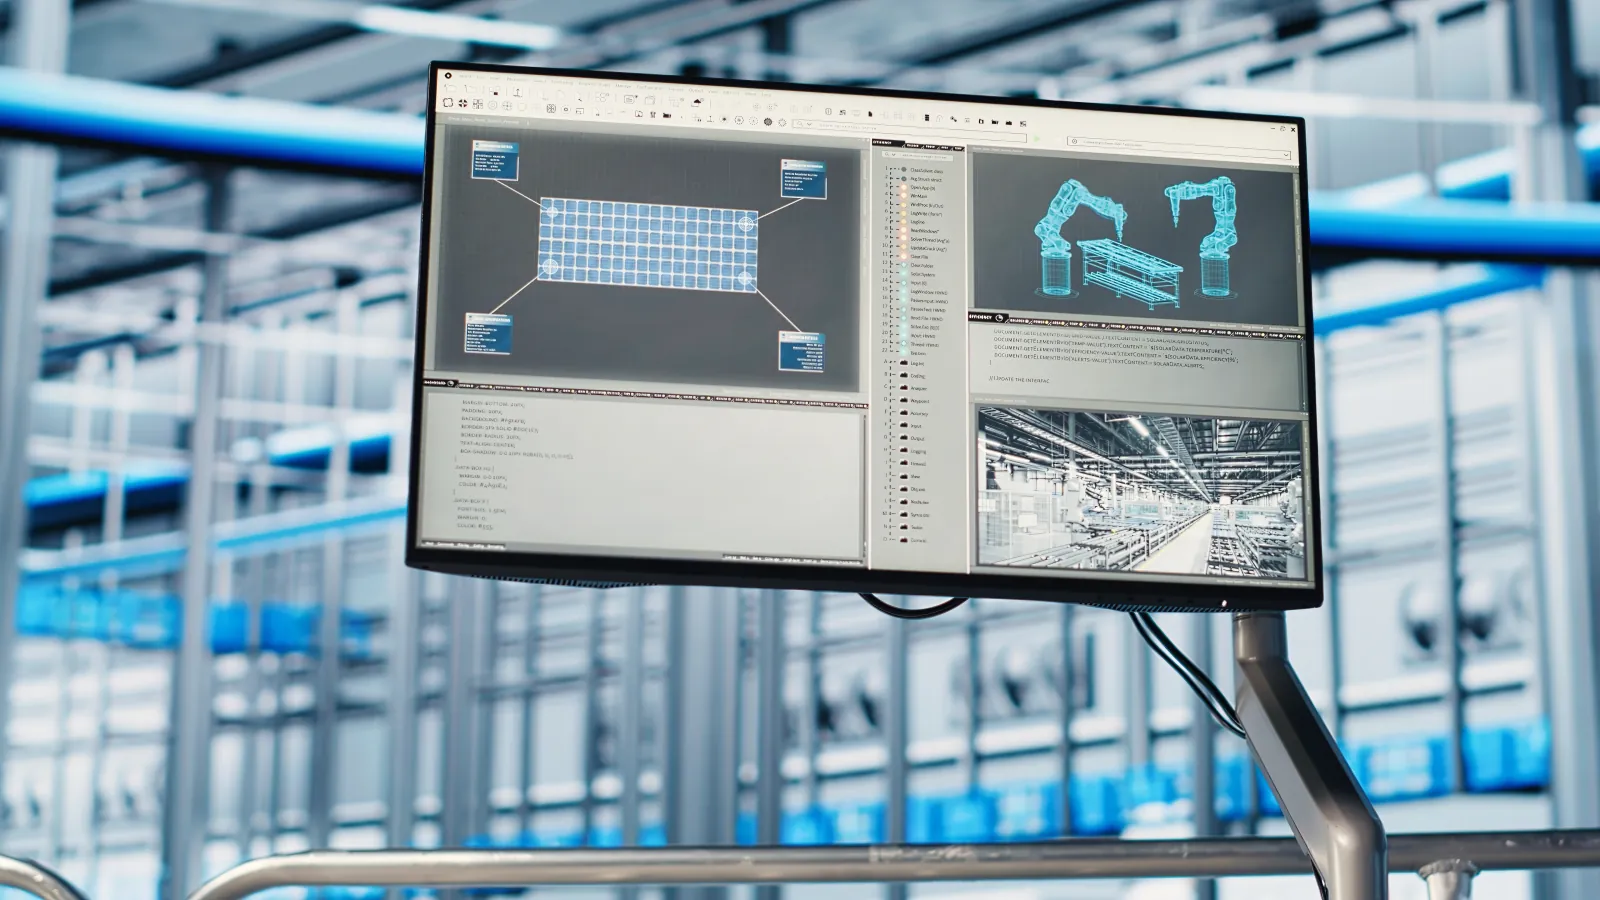
We develop SCADA systems, network your machines and bring machine states, process values and production key figures together in shared dashboards.
Clear display of machines, stations and lines. States, current values and fault messages can be assigned directly to the affected area.
Bundling data from several controllers in one dashboard. Trend curves and agreed key figures show how individual installations and the entire production are developing.
Changing authorised setpoints, sending operating commands and acknowledging faults where applicable. We define user rights, permissible values and authorisations for each project.
Machine data acquisition and production data analysis
Which machine is at a standstill, where is production time lost and how is the cycle changing? We network machines and acquire the available production data automatically. Your team sees the running times, downtimes and quantities of all machines in one evaluation.
Connecting individual machines, stations and lines via existing interfaces. We define with you which data points go where.
Automatically acquiring states, quantities, cycle times and process values and storing them with a time reference. We check which values are available on your controllers.
Evaluating running times and downtimes by machine and time period. If the controller supplies fault causes or they are added, you see which interruptions recur.
Comparing key figures in the production dashboard and evaluating process trends. This lets you identify cycle deviations and see where you need to take a closer look.
Robot, PLC and process tool as one cell sequence
We develop the process path, state logic, diagnostics and version management together. Product changes, troubleshooting and restart remain traceable for operation and maintenance.
- Process pathTool and base calibration, gripping points, process paths and motion profile
- State logicPLC handshake, peripheral signals, recipe and variant selection
- DiagnosticsError handling, safe retraction moves and guided restart
- Version managementCycle time optimisation, program backup, version status and documentation
How we structure PLC and SCADA programs
Structured programs, defined data points and documented changes help your maintenance team find their way around the program. Later extensions build on this basis.
Structured PLC functions, clear designations, comments and documented interfaces make troubleshooting and later extensions easier.
We remain available for adjustments, optimisation and fault analysis. We agree access and the required licences with you in advance.
Project process and technical handover
We define the control and data scope, program the PLC and SCADA and test every agreed function on your installation. We document programs, tests and handover.
Recording controllers, data and objectives
We record PLCs, user interfaces, existing programs and interfaces. We then define with you which functions will be created, who gets access and when we intervene in ongoing production.
Programming PLC and SCADA
We program sequence control, plant networking and visualisation so that they fit together. In doing so, we define data points, messages and operating rights.
Testing functions on the installation
We test signals, operating modes, data transmission and typical fault scenarios. Safety validation follows as a separate step.
Handing over programs and instructing your team
You receive backups, parameters, version statuses and the documentation. We instruct your team and record open points and next steps.
Frequently asked questions about PLC, SCADA and machine data
Answers on PLC programming, SCADA development for several installations and what machine data can tell you.
What tasks do you take on in PLC programming?
We develop and modify step sequences, operating modes, interlocks and the control of sensors, actuators and peripherals.
This also includes station interfaces, recipes, HMI functions, diagnostics and restart. How far we can intervene depends on the controller, program access and documentation.
Do you also reprogram existing PLCs?
Yes, we modify and extend existing PLC programs. To do so, we check the existing programs, access and interfaces and then implement the machine functions you need.
Before we intervene, we back up the old program version and agree with you on downtime windows, test conditions and the way back.
Do you program Beckhoff controllers with TwinCAT 3?
Yes. We program Beckhoff controllers with TwinCAT 3, either new or as an extension of existing programs. This includes sequence control, EtherCAT peripherals, drives, operation and diagnostics.
We clarify which controller, which TwinCAT version and which program access you have before we send you a quotation.
Can you migrate older controllers to TwinCAT, S7-1200 or S7-1500?
Yes, as a control system migration in a retrofit. We back up the program version and decide with you, based on the peripherals and your team, whether an S7-1200 or S7-1500 with ET 200SP in TIA Portal or a current Beckhoff controller with TwinCAT 3 is the right fit.
We transfer S5 and S7 programs to TIA Portal with the Siemens converter and rebuild blocks that cannot be converted in SCL. We then test on the machine and hand over the program version and documentation.
Our Knowledge article PLC migration to S7-1500 describes the process, risks and downtime.
Do you program Siemens controllers in TIA Portal?
Yes. We program Siemens controllers in TIA Portal, either new or as an extension of existing programs. This includes sequence control, peripherals, drives, operation and diagnostics.
We clarify which controller, which TIA Portal version and which program access you have before we send you a quotation.
What do SCADA programming and SCADA development mean?
SCADA stands for Supervisory Control and Data Acquisition: higher-level software for monitoring, data acquisition and authorised operation of installations.
We develop the user interface, integrate the available controller data and implement the agreed messages, trends, evaluations and operating functions.
How do you network machines with different controllers?
On each controller, we check which interfaces, access options and data points are available. We then define how machines, stations and lines deliver data to the shared system.
A uniform assignment of machines, states and time references makes the data comparable. Before implementation, we tell you which existing installations can be integrated and what needs to be changed for this.
What does machine data acquisition contribute to production evaluation?
Machine data acquisition (MDA) provides technical data such as machine states, running times, downtimes, quantities and cycle times. In the production dashboard, you can compare these values by machine and time period.
We define the key figures, data sources and evaluations with you. You see where and for how long machines are at a standstill, as precisely as the available data allows.
Can I operate installations via the SCADA dashboard?
Yes. We build authorised setpoints, operating commands and fault messages into the dashboard, and where permissible also acknowledgement.
We define user rights, permissible values and authorisations for each project. Required safety functions remain the task of the machine control system.
How do MDA, condition monitoring and predictive maintenance differ?
MDA records machine data. Condition monitoring monitors the condition on the basis of measured values and trends. Predictive maintenance uses suitable data to derive indications of future maintenance needs.
We derive forecasts and sound statements from the actual installation data and check them against that data. Data acquisition alone is not enough for a sound failure prediction.
Does SCADA run in the browser or on the machine PC?
Both are possible: in the browser within your company network or as a local application on the machine PC.
Before development, we agree with you on operation, data storage, access rights, documentation and the required licences.
Discuss a PLC or SCADA project
A new PLC program, networked machines or a dashboard for production data: show us your installations and describe what should work at the end. We check controllers and interfaces and tell you the scope for PLC, SCADA and MDA.
Simon Niklas
Mechanical engineer, M.Sc.
+49 941 56956720[email protected]
“Good engineering proves itself in day-to-day production. That is why we combine technical planning with a close understanding of process, operation and maintenance.”
Book a consultation